
What Is the Best Magnet Type for 3D Prints?
When deciding what magnets do you use for 3D prints, the short answer is almost always neodymium (NdFeB) rare-earth magnets. 3D printed assemblies usually have tight space constraints, thin walls, and precise tolerances. You need maximum holding power in the smallest possible footprint, and neodymium delivers the highest magnetic strength per cubic millimeter of any commercially available material.
While neodymium handles 90% of maker projects, other materials have niche roles depending on budget, heat exposure, and overall part volume.
| Magnet Type | Pull Strength | Size Profile | Best 3D Print Application |
|---|---|---|---|
| Neodymium (NdFeB) | Extremely High | Ultra-compact | Lids, tool holders, quick-release mounts, miniatures |
| Ferrite (Ceramic) | Low to Moderate | Bulky | Large workshop fixtures, low-cost fridge novelty prints |
| Samarium Cobalt (SmCo) | High | Compact | High-heat engine bays, heated printer chambers (>150°C) |
| Flexible Rubber/Strips | Very Low | Flat / Sheet | Swappable signage, light decorative panels |
Neodymium magnets: the usual choice for compact parts
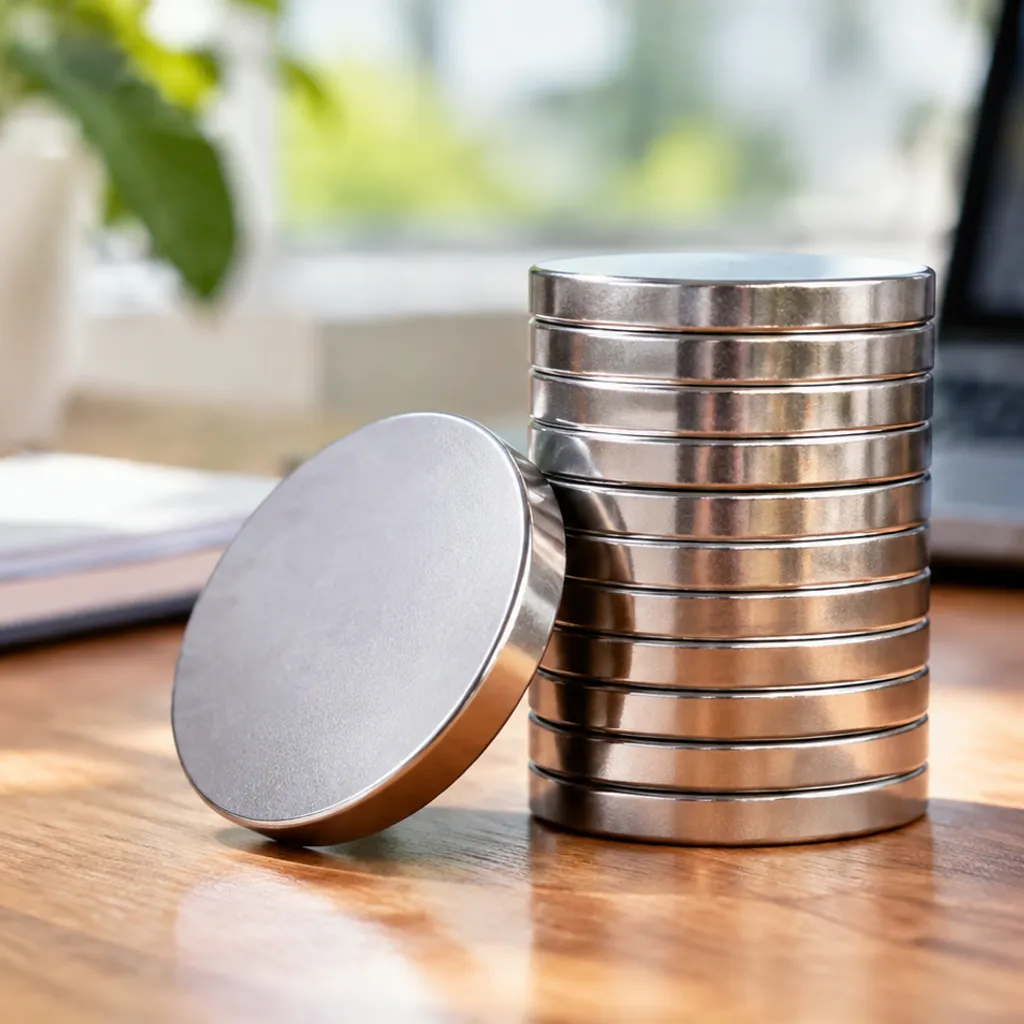
Neodymium magnets for 3D printing are the industry standard for functional prints. Because 3D printed walls add distance between mating magnetic faces, you need strong field penetration to bridge that gap.
-
- Maximum force in tight spaces: A tiny 6x3mm disc magnet can hold a print enclosure door shut without adding unnecessary bulk to your CAD model.
- Predictable standard sizes: Standard disc shapes drop cleanly into round slicer-generated pockets without requiring custom geometry.
- Secure mechanical engagement: Their strong pull provides an authoritative, satisfying snap for modular accessories, removable lids, and swappable printer toolheads.
Ferrite magnets: when a larger, lower-cost magnet may work
Ferrite (ceramic) magnets offer a fraction of the pull force of rare-earth magnets. In a direct ferrite vs neodymium magnets comparison, a ferrite block must be several times larger to match the holding power of a standard neodymium disc.
-
- Budget-driven bulk prints: Ferrite costs significantly less when producing large quantities of non-critical items.
- Corrosion resistance: Ferrite does not rust when exposed to moisture or outdoor environments, even without protective plating.
- Design penalty: You must model thick, bulky housings to fit them, making them impractical for compact or sleek 3D printed parts.
Other magnet types and when to consider them
Beyond standard discs and blocks, specific projects demand specialized magnetic materials:
-
- Samarium Cobalt (SmCo): When we design functional parts that operate inside heated enclosures, near hotends, or around automotive engines, standard neodymium loses its magnetic strength quickly. SmCo handles extreme temperatures well above 250°C without permanent loss of magnetic pull.
- Flexible magnetic sheets: These work well for 3D printed flat signs, modular board game tiles, or magnetic baseplates. While they lack the clamping force for structural load, they are easy to cut, shape, and adhere directly to flat printed surfaces.
How to Choose a Magnet for a 3D-Printed Part
When deciding what magnets do you use for 3D prints, picking the right hardware comes down to four core design decisions. We always match mechanical load, physical geometry, and working environments before slicing a model.
Start with the Job the Magnet Needs to Do
Every functional print places different physical demands on a magnetic joint:
-
- Tactile positioning: Light snapping lids, fidget sliders, or board game tiles only need low-power holding to locate parts.
- Enclosures and latches: 3D printed enclosure doors require enough pull force to resist minor vibrations without making the door difficult to pull open.
- Load-bearing mounts: Tool racks, pegboard holders, and wall fixtures need maximum retention force to counter continuous shear and gravity.
Choose the Shape and Dimensions
Physical form dictates how you model cavities in your CAD software:
-
- Disc magnets for 3D printing: Cylindrical discs are the easiest to integrate. Round pockets print cleanly with standard slicer hole compensation and don’t require corner clearance adjustments.
- Rectangular blocks: Best for linear tracks, sliding latches, or thin flat edges where round magnets would compromise the print wall thickness.
- Countersunk rings: Ideal when you want to secure the magnet mechanically using a flat-head screw directly into an insert or threaded hole, bypassing glue entirely.
Understand Magnet Grade and Holding-Force Claims
Magnet grade defines magnetic energy density. Higher numbers produce more magnetic field strength for the exact same physical size.
| Magnet Grade | Relative Strength | Best Use Case in 3D Printing |
|---|---|---|
| N35 | Moderate | Lightweight covers, tabletop miniatures, alignment stops |
| N42 | High (Balanced) | Everyday functional brackets, tool caddies, swappable parts |
| N52 | Maximum | Compact spaces requiring maximum grip through embedded plastic layers |
Manufacturer pull ratings reflect ideal bench tests against raw, thick steel. In practical 3D printing, plastic gaps, print layer textures, and lateral shearing forces will reduce effective holding force.
Consider Coating and Environment
Raw magnet material rusts quickly if exposed to the air. Standard rare-earth magnets for 3D prints feature a triple-layer Nickel-Copper-Nickel (Ni-Cu-Ni) coating, which works well for indoor applications. For humid or outdoor settings, look for epoxy or plastic-coated options to prevent moisture intrusion.
Heat limits are equally critical. Standard neodymium grades permanently lose magnetic strength when exposed to temperatures above 80°C (176°F). Similar to the selection factors detailed in our guide on how to choose the right magnet for your appliances, verifying the thermal envelope ensures your magnets withstand heated printer enclosures, hot car interiors, or warm mechanical housings without degaussing.
How Much Holding Force Do You Need?
When deciding what magnets do you use for 3D prints, holding force is usually the first spec makers look at. However, relying purely on the advertised rating on a spec sheet often leads to latches that pop open or tool holders that slide right off. Calculating the required magnetic retention for magnets for 3D printed parts means accounting for working loads, gravity, and the mechanical leverage acting against the joint.
Real-World Holding Force vs Theoretical Pull Force
The advertised pull force from manufacturers reflects an absolute ideal scenario: vertical separation from a flat, ground-steel plate with zero gap. In functional printing projects, your parts operate in far messier conditions.
When evaluating what is a magnetic force in a practical assembly, the actual usable grip depends on the contact surface and pull angle:
| Condition | Theoretical Rating | Real-World Output | Practical Application Impact |
|---|---|---|---|
| Direct Pull (Magnet to Steel) | 100% | 70% – 90% | Good for direct vertical lids and magnetic latches. |
| Magnet-to-Magnet Contact | 100%+ | 85% – 95% | Strongest alignment, but requires matched polarity. |
| Shear Force (Sliding sideways) | 100% | 15% – 30% | Magnets slide easily on smooth plastics without mechanical stops. |
| Embedded (Through 0.8mm wall) | 100% | 20% – 40% | Magnetic flux drops off sharply with distance. |
Key Factors That Weaken Magnetic Grip in Prints
We regularly see parts fail not because the magnet was defective, but because the print geometry compromised the magnetic field:
-
- Plastic Layer Gaps: Every 0.2 mm layer line between mating faces acts as an air gap. A print covering a magnet with just two perimeter walls can cut usable pull strength by more than half.
- Shear Loads: Neodymium magnets resist pulling forces well, but slide effortlessly across smooth surfaces. If your print experiences lateral force, add physical alignment pins, ribs, or interlocking lips to handle the shear load.
- Layer Line Texture: Standard FDM print surfaces are not perfectly flat. The microscopic ridges reduce direct contact area, further lowering retention.
- Mating Metal Thickness: If you attach a magnet to a standard screw head or thin sheet metal, the metal saturates quickly and cannot absorb the full magnetic field, leaving you with weak retention.
Prototyping Margins for Functional Parts
To prevent functional failures, we apply clear design margins based on the magnet grade and holding force required for the task:
-
- Light Snap Lids and Miniatures: Size for 2x the expected component weight. A standard 5×2 mm or 6×2 mm disc magnet handles light enclosure doors easily.
- Tool Mounts and Heavy Fixtures: Size for 4x to 5x the total weight. This safety factor counteracts vibrations, bumping, and shear slip.
- Print Quick Test Strips: Never commit to a multi-hour print before testing your fit. Print a 15-minute test strip containing three different pocket sizes and test the physical grip against your actual mating surface first.
Designing Magnet Pockets in a 3D Print
Getting the pocket design right makes or breaks your build. When you evaluate what magnets do you use for 3D prints, pocket geometry is just as critical as the magnet itself. A pocket that is too tight cracks your layer lines during insertion, while an oversized slot lets the magnet pull free under its own attraction.
Allow for Fit and Manufacturing Variation
FDM printers naturally squish filament slightly outward on horizontal perimeters (XY expansion). Slicing a nominal 6 mm hole for a 6 mm disc magnet will always produce a tight, failed fit. We design our 3D printed magnet pockets with clear radial offsets tailored to the installation method.
| Installation Style | Magnet Diameter Offset (XY) | Pocket Depth Offset (Z) | Typical Use Case |
|---|---|---|---|
| Press-Fit | +0.05 mm to +0.10 mm | +0.00 mm to +0.10 mm | Friction-locked mechanical retention |
| Glued (Adhesive) | +0.20 mm to +0.30 mm | +0.20 mm (glue gap) | Removable lids, high-shear applications |
| Fully Embedded | +0.30 mm to +0.40 mm | +0.20 mm to +0.40 mm | Enclosed prints paused mid-cycle |
Choose a Pocket Depth and Wall Thickness
Magnetic flux drops off sharply with distance according to the inverse-square rule. Even a thin layer of plastic between two magnets significantly degrades holding strength:
-
- Mating Face Wall Thickness: Keep the barrier between mating magnets down to 0.4 mm–0.8 mm (1 to 2 line widths). Going thicker than 1.2 mm drastically weakens the grip.
- Structural Backing: Maintain at least 1.2 mm to 1.6 mm of solid infill or perimeters behind the magnet pocket to prevent the magnet from ripping through the back wall under tension.
- Flush Mounting: For direct magnet-to-magnet contact, size the depth so the magnet sits 0.1 mm below the print surface. This protects the brittle plating from direct impact damage while maximizing pull force.
For projects relying on multi-magnet arrays or rotational alignment, reviewing a magnetic coupling types and selection guide provides practical insight into how spacing and array layouts influence mechanical transfer.
Plan Polarity and Orientation
Reversing a magnet inside an embedded or glued pocket ruins the print. We follow a strict polarity control process before pressing parts together:
-
- Keep a Master Reference Magnet: Mark the north pole of a dedicated setup magnet with bright paint or permanent marker.
- Mark Every Magnet Before Assembly: Touch each magnet to your reference block and dot the exposed side with a marker so polarity is obvious at a glance.
- Use a 3D Printed Insertion Jig: Print a small plastic push-stick with an embedded magnet oriented in the reverse direction. This holds your target magnet flat and drives it straight into the pocket with the correct face forward every time.
Three Ways to Install Magnets in 3D Prints
Choosing what magnets do you use for 3D prints is only half the battle; how you mount them determines whether your part holds up under repeated use. We rely on three primary installation methods depending on the mechanical stress, aesthetic needs, and printer setup.
Pause the Print and Embed the Magnet
Embedding locks the magnet completely inside the print. It produces a seamless, factory-molded look and keeps the magnet from ever pulling out of its socket.
-
- Slicer pause: Add a pause command at the final open layer of the cavity before bridging begins.
- Nozzle clearance: Add at least 0.2 mm vertical clearance above the magnet so the hotend does not collide with it when resuming.
- Ferrous attraction risk: Standard steel nozzles will attract loose magnets out of the slot as the printhead passes over. Secure the magnet with a drop of glue or hold it down with blue painter’s tape before resuming.
- Thermal limits: Standard neodymium magnets can lose strength if heated bed temperatures exceed 80°C for extended periods. For high-temperature enclosures or specialized builds, understanding what are the grades of SmCo magnets helps when standard rare-earth grades cannot survive the ambient chamber heat.
Press-Fit the Magnet After Printing
A pure mechanical fit avoids adhesives and allows for fast assembly directly off the print bed.
-
- Pocket tolerances: Design the pocket diameter with an interference fit of roughly +0.05 mm to +0.1 mm over the actual magnet size, depending on printer calibration.
- Lead-in chamfer: Model a 0.5 mm, 45-degree chamfer at the mouth of the hole. This prevents the magnet from peeling layers as it enters.
- Insertion tools: Press the magnet in place using a parallel vise, arbor press, or flat pliers rather than tapping it with a steel hammer, which can shatter brittle sintered magnets.
- Material choice: Tougher filaments like PETG, ABS, and nylon tolerate press-fitting well. Rigid PLA is prone to micro-cracking along layer lines if the pocket is too tight.
Glue the Magnet into a Pocket
Adhesive mounting is the most forgiving method regarding dimensional variation and allows post-print polarity corrections.
-
- Pocket clearance: Model cavities with a loose slip-fit (+0.15 mm to +0.25 mm clearance on all sides) to provide space for the glue layer.
- Recommended adhesives: Medium-viscosity cyanoacrylate (CA glue) bonds quickly to bare PLA and PETG. For high-impact closures or shearing forces, a slow-cure two-part epoxy creates a significantly stronger, shock-resistant bond.
- Surface prep: Nickel-plated magnets are slick. Lightly scuffing the bottom surface of the magnet with 220-grit sandpaper gives the adhesive a rough surface to bite into.
- Polarity verification: Mark matching poles with a permanent marker before applying glue. Once standard CA glue or epoxy cures, extracting a reversed magnet usually ruins the 3D-printed part.
How Printing Material and Temperature Affect Magnet Choice
When deciding what magnets do you use for 3D prints, heat tolerance and filament behavior dictate your success. Standard neodymium magnets lose their magnetic strength quickly when exposed to temperatures common in 3D printing and heated enclosures.
Operating Temperatures vs Printing Temperatures
Standard neodymium (NdFeB) magnets carry an “N” rating (such as N42 or N52) and feature a maximum operating temperature of 80°C (176°F). Pushing them past this limit causes permanent loss of magnetic pull force.
-
- Heated beds: Printing ABS, ASA, or Nylon requires bed temperatures between 90°C and 110°C. Embedding a standard N-grade magnet directly against the bottom layers will degrade its field strength before the print finishes.
- Nozzle contact: Molten plastic exits at 200°C to 280°C, but brief contact during bridging generally will not overheat the magnet core.
- Ambient chamber heat: Active heated chambers can easily cross the 80°C threshold, making standard neodymium unsuitable.
| Magnet Grade Suffix | Max Operating Temp | Ideal Filament Match |
|---|---|---|
| Standard (N) | 80°C (176°F) | PLA, PETG, TPU |
| M | 100°C (212°F) | High-temp PETG, lightweight ABS |
| H | 120°C (248°F) | ABS, ASA, PC-ABS blends |
| SH | 150°C (302°F) | Nylon (PA), Polycarbonate (PC) |
Filament Shrinkage and Thermal Pocket Stability
Different 3D printing filaments shrink at different rates as they cool from extrusion temperature to room temperature. This directly impacts the fit of your magnet pockets:
-
- PLA: Shrinks minimally (0.2%–0.4%). Magnet pockets stay true to CAD dimensions with standard clearances (0.10 mm to 0.15 mm).
- PETG: Moderate shrinkage and slight flex. Great for press-fit designs because the material yields slightly without snapping.
- ABS / ASA: High shrinkage (1.0%–1.8%). If you size a pocket too tight, thermal contraction will squeeze the magnet and cause perimeter layer separation or visible outer-wall bulging.
- Reinforced Filaments (CF/GF): High stiffness with low thermal shrinkage, but zero flexibility. Press-fits require wider offsets to avoid cracking brittle pocket walls.
Preventing Permanent Demagnetization Under Heat
Heating a magnet past its maximum operating temperature causes irreversible flux loss. Much like evaluating the difference between surface permanent magnet and interior permanent magnet layouts for thermal stability in mechanical systems, enclosing a magnet within dense plastic creates an insulating barrier that traps heat.
To protect your magnets during hot builds:
-
- Select high-temperature grades: Specify SH (up to 150°C) or UH (up to 180°C) neodymium magnets for prints subjected to warm engine bays, direct summer sun, or heated build chambers.
- Increase pause efficiency: When embedding magnets mid-print, insert them immediately before resuming to minimize exposure time to the heated bed.
- Use secondary installation: For parts printed in high-temp filaments like PC or Nylon, leave an open pocket and glue or press the magnet in after the print has cooled completely to room temperature.
Common Mistakes to Avoid
Integrating magnets into prints looks simple until a part splits, a polarity flips, or a latch refuses to hold. When we evaluate failed assemblies, the issues almost always trace back to a few avoidable design and installation oversights.
Relying on Grade Ratings Instead of Physical Dimensions
A common misconception is that stepping up from an N35 to an N52 grade will double your holding force. Material grade only represents magnetic energy density—it typically yields a modest 10% to 20% bump in grip for the same footprint.
-
- Volume beats grade: Increasing a disc magnet’s diameter from 6mm to 8mm or adding 1mm of thickness provides a far greater increase in pull force than buying a higher grade.
- Match grade to application: Standard grades handle everyday latches, while high-temperature NdFeB magnets UH grade are engineered specifically for thermal stability under high operating heat rather than sheer pull force alone.
Neglecting Printer Clearance and Pocket Tolerances
Designing a pocket at the exact nominal size of the magnet guarantees a failed fit. FDM printers naturally squeeze molten filament outward, resulting in inner-diameter shrinkage.
-
- Account for printer offset: Always add a +0.10 mm to +0.20 mm diametrical clearance to your 3D printed magnet pockets to ensure a clean drop-in or smooth press-fit.
- Avoid post-print drilling: Drilling into cured prints often blows out the bottom floor or tears weak layer lines. Calibrate your magnet pocket tolerance directly in your CAD model.
Mixing Up Magnet Polarity During Installation
Nothing ruins a multi-part print faster than installing a magnet backward so the mating pieces repel each other. Once cyanoacrylate adhesive sets, removing the magnet without destroying the plastic is nearly impossible.
-
- Mark your reference stack: Keep your supply in a single stack and mark the top pole of every magnet with a permanent marker.
- Use an assembly jig: Use an existing mating part or a dedicated alignment tool to press the magnet into place. This physically prevents reverse installation before the glue bonds.
Thick Plastic Barriers Between Mating Surfaces
Magnetic force drops off sharply over distance following the inverse-square law. Embedding a magnet beneath thick infill or top layers significantly degrades holding power.
-
- Limit face layers: If you embed magnets beneath a solid top skin, keep the covering shell between 0.4 mm and 0.8 mm (one to two perimeters or top layers).
- Prioritize flush contact: Direct magnet-to-magnet contact delivers 100% of the rated holding strength. Every additional 0.5 mm of plastic barrier can cut usable pull force by more than half.
Cracking Thin Print Walls with Oversized Magnets
Pressing an interference-fit magnet into an undersized pocket places heavy tensile stress perpendicular to the layer lines, leading directly to delamination.
-
- Reinforce surrounding walls: Maintain a minimum exterior wall thickness of 1.2 mm to 1.6 mm (3 to 4 perimeters) around any magnet pocket.
- Distribute insertion force: Never strike rare-earth magnets directly with a metal hammer. Use an arbor press, a smooth-jaw clamp, or hand pressure against a flat surface to seat the magnet evenly without fracturing the surrounding print walls.
Magnet Safety for 3D Printing Projects
When deciding what magnets do you use for 3D prints, rare-earth neodymium discs are almost always the top choice. However, their high pull force brings specific workshop hazards that we need to manage during printing and assembly.
Pinch Risks and Brittle Impact Chipping
Neodymium magnets are sintered metal ceramics. They are remarkably strong but extremely brittle.
-
- Skin Pinches: Uncontrolled snapping between two bare magnets can easily pinch skin and cause blood blisters.
- Shattering Shards: When two magnets slam together at high speed, they do not bend—they shatter. Flying sharp flakes can cause eye injuries.
- Separation Technique: Always slide magnets apart sideways from a stack rather than pulling them straight off.
- Eye Protection: Wear basic safety glasses when working with stacks of magnets larger than 10 mm in diameter.
Swallowing Hazards for Children and Pets
Loose rare-earth magnets pose a severe, life-threatening internal hazard if swallowed:
-
- Internal Pinching: If more than one magnet is ingested, they attract through intestinal walls, cutting off blood flow and causing rapid perforations.
- Design Precautions for 3D Prints: Never use exposed press-fit or surface-glued magnets for children’s toys, pet accessories, or loose household items.
- Embedded Enclosures: For any print that might enter a household environment, we always seal the magnets inside solid plastic walls using the pause-and-insert printing method so they cannot dislodge over time.
Shielding Sensitive Electronics and Media Storage
Strong localized magnetic fields can disrupt nearby hardware during both printing and everyday use:
-
- Printer Components: Keep strong magnets clear of your printer’s stepper motors, inductive bed-leveling probes, and Hall-effect endstops during assembly.
- Data and Devices: Keep bare magnets away from mechanical hard drives, magnetic stripe cards, and pacemakers.
- Dynamic Setups: Just as precise placement is critical when applying magnetic solutions for wobbling fixtures, ensure magnets embedded near rotating shafts or enclosed sensors maintain enough clearance to avoid unwanted electromagnetic drag or erratic readings.
What to Check When Buying Magnets for 3D Prints
When we source magnets for 3D printed parts, minor manufacturing deviations can ruin an entire print run. A magnet pocket designed around exact digital specs will fail if the physical parts arrive oversized or underpowered. Here is our checklist to ensure you get consistent hardware every time.
Verifying exact dimensions, coatings, and material grades
Never design around advertised nominal sizes alone. Budget suppliers often list nominal dimensions that deviate significantly from real-world batches.
-
- Actual Dimensions vs. Nominal: Always measure sample lots with digital calipers. An “8×3 mm” disc often arrives at 7.85 mm or 8.15 mm. A pocket designed without checking these deviations leads to failed press-fits or loose cavities.
- Protective Coatings: Standard neodymium magnets for 3D printing typically feature a triple-layer Ni-Cu-Ni (nickel-copper-nickel) plating. If your printed enclosures face moisture or high friction, look for epoxy, rubber, or plastic coatings to prevent premature flaking and corrosion.
- Verified Material Grade: Confirm the grade rating (e.g., N35, N42, or N52). Higher grades deliver greater magnetic flux in tight spaces, which is just as critical here as it is when selecting what magnet materials are best for Halbach arrays and compact motor assemblies.
Checking working temperature limits and pull test methods
Standard rare-earth magnets quickly lose their magnetic field if exposed to heat beyond their rating.
| Magnet Suffix | Max Operating Temperature | Recommended 3D Printing Use Case |
|---|---|---|
| Standard (No suffix) | 80°C (176°F) | Ambient PLA prints, display models, standard latches |
| M | 100°C (212°F) | Heated bed contact zones, enclosed ABS/PETG parts |
| H / SH | 120°C – 150°C (248°F – 302°F) | Enclosed builds, automotive mounts, heated functional tools |
Check how the supplier tests pull force. Advertised holding force is almost universally measured on a ground, flat steel plate in direct contact under laboratory conditions. Sliding force (shear) is usually only 15% to 30% of direct vertical pull force, so factor this reduction into your enclosure latches.
Sourcing batch consistency for repeatable production
If you run batch production or print modular assemblies, consistency matters more than raw strength.
-
- Uniform Outer Diameters: A run of 100 disc magnets for 3D printing should hold a tolerance within ±0.05 mm. Broader swings will force you to re-calibrate slicing tolerances between print jobs.
- Axial Polarity Alignment: Ensure the supplier packages axial magnets stacked cleanly in a column with matching orientation. Jumbled bulk bags make it easy to mix up north and south poles during rapid assembly runs.
- Reputable Sourcing: Avoid unbranded, multi-vendor marketplaces for functional prototypes. Buy from dedicated magnet vendors who publish verified technical data sheets, working temperature ceilings, and genuine flux ratings.
Frequently Asked Questions
Are neodymium magnets the best choice for most 3D prints?
Yes. When makers ask what magnets do you use for 3D prints, neodymium magnets (NdFeB) are almost always the answer. They deliver the highest pull force per millimeter of space, making them the industry standard for 3D printed enclosure magnets, tool holders, and modular prints where internal cavity space is limited. Ferrite magnets are far too weak and bulky for compact functional parts.
Can you pause a 3D print to add a magnet?
Yes. Pause-and-insert magnet printing is one of the cleanest ways to conceal hardware inside a print.
Add a pause command at the target layer in your slicer just before the cavity roof closes.
Drop the magnet into the cavity.
Ensure the magnet sits completely flush or slightly sub-flush to avoid colliding with the nozzle.
Secure the magnet with a drop of glue so the magnetic pull from a steel nozzle does not yank the magnet out of the pocket before the printer bridges the top layer.
How much clearance should a magnet pocket have?
For standard FDM setups, we recommend a magnet pocket tolerance of +0.10 mm to +0.20 mm on the pocket diameter and +0.10 mm to +0.15 mm on pocket depth. This accommodates standard perimeter expansion, corner bulging, and typical manufacturing variances in disc magnets for 3D printing.
Can a 3D-printed magnet pocket be press-fit?
Yes, but filament selection matters:
PETG and ABS: Ideal for press-fit magnets in 3D prints because these materials flex slightly without splitting along layer lines.
PLA: Extremely stiff and brittle. Forcing an oversized magnet into a tight PLA cavity frequently causes layer delamination or cracks along thin perimeter walls.
Design tip: Add a 0.2 mm lead-in chamfer to the mouth of the pocket so the magnet starts straight under pressure.
Which adhesive works for attaching magnets to a print?
Standard smooth nickel platings give adhesives very little physical grip. We use two main bonding solutions:
Cyanoacrylate (Super Glue): Best for quick light-duty assemblies. Use medium or gel viscosity to prevent run-off into functional mechanisms.
Two-Part Epoxy: The gold standard for mechanical parts subjected to repeated snapping or shear stress.
Surface prep: Always lightly scuff the contact face of the magnet with 220-grit sandpaper to give the adhesive mechanical purchase.
Does a stronger magnet grade always mean better results?
Not necessarily. While an N52 magnet yields higher theoretical flux than an N35, physical geometry and separation distance matter far more. A thick plastic layer between mating parts degrades pull force faster than an upgraded grade can compensate for. Maximizing contact surface area and keeping plastic barriers under 0.6 mm will do more for holding power than simply buying higher-grade rare-earth magnets for 3D prints.
Can magnets be used in parts exposed to heat or moisture?
Standard N-grade neodymium magnets permanently lose their magnetic charge if exposed to temperatures above 80°C (176°F). For heated enclosures, automotive interiors, or high-temperature builds, look for high-temp ratings (such as SH or UH classes), similar to the thermal limits encountered when studying what type of magnets are used for microwave magnets. For wet or outdoor environments, use epoxy-coated magnets, as standard nickel coatings can scratch, allowing moisture inside to oxidize and destroy the core NdFeB material.
Related Links
https://forum.bambulab.com/t/magnets-in-prints/76022
https://www.microcenter.com/site/mc-news/article/3d-printing-hardware.aspx
 English
 German
 Vietnamese
 Spanish (Mexico)
 Russian
 Turkish
 Polish
 Hindi
 Thai
 Malay
 Korean
 Japanese
 French
 Czech
 Danish
 Dutch
 Finnish
 Italian
 Portuguese (Brazil)
 Portuguese (Portugal)
 Slovenian
 Ukrainian
 Hebrew
 Scottish Gaelic
 Hungarian
 Tagalog
 Spanish (Spain)
 Serbian
 Indonesian
 Slovak
 Dutch (Belgium)
 Persian
 Arabic
 Romanian
 Estonian
 Greek
 Bulgarian
Leave A Comment